Fabricante de impressoras de jato de tinta pequeno de tamanho pequeno
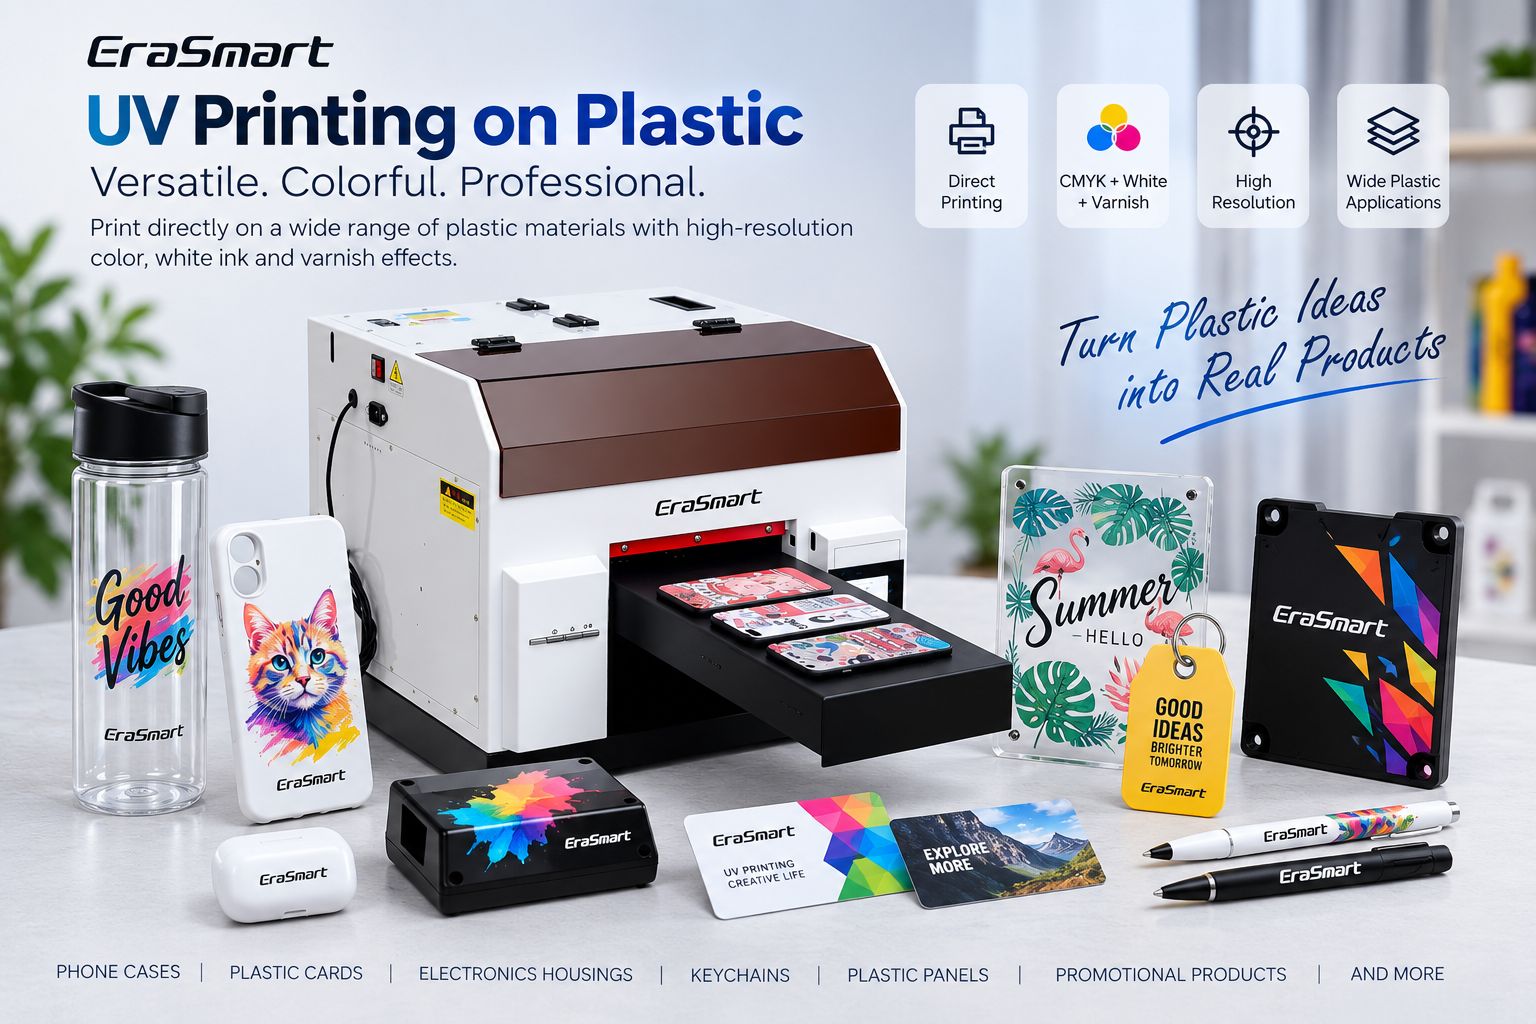
Impressora UV ERASMART para impressão de plásticos
UV printing makes it possible to print full-color graphics, white ink and decorative varnish effects directly onto many plastic products.
As aplicações típicas incluem:
- Casos de telefone
- plastic cards
- electronics housings
- chaveiros
- etiquetas
- control panels
- produtos promocionais
- plastic signs
- amostras de embalagem
- cosmetic containers
- custom panels
But there is one important rule every UV printer buyer and operator should understand:
Plastic is not one material.
ABS, PVC, polycarbonate, PET, TPU, polypropylene and polyethylene can behave very differently with the same UV ink.
A design that adheres well to an ABS phone-case blank may perform poorly on a polypropylene container. A PVC card may print easily while a polyethylene bottle made with a different resin formulation may need additional surface treatment.
EraSmart’s current UV Printer Materials Guide therefore classifies plastic suitability as “varies by type” and recommends testing the exact plastic product before production.
The most reliable production workflow is:
Identify the plastic → inspect the surface → clean → test direct printing → evaluate pretreatment if required → print a sample → test adhesion → standardize → begin production
Quick Answer: Can a UV Printer Print on Plastic?
Yes, but not every plastic is equally easy to print.
Some plastics commonly provide more workable surfaces for UV ink, while others are more challenging and may require primers, coatings, corona treatment, plasma treatment or another validated surface-preparation method.
| Plástico | Typical Printing Situation | Main Consideration |
|---|---|---|
| ABS | Often workable | Surface cleanliness |
| PVC | Often workable | Formulation and coating |
| Polycarbonate / PC | Often workable | Cleaning and surface treatment |
| PET / PETG | Varies | Tratamento de superfície |
| TPU | Dependente do aplicativo | Adhesion + flexibility |
| PP | Mais desafiador | Low surface energy |
| PE | Mais desafiador | Low surface energy |
| Coated plastic | Depends on coating | Ink-to-coating adhesion |
Technical inkjet guidance also shows why a single “plastic compatibility” claim is misleading: PET, ABS, PVC and polycarbonate can show good adhesion in some UV ink systems, while PP and PE are often specifically identified as more difficult substrates.
So instead of asking:
Can a UV printer print plastic?
Perguntar:
What exact plastic is this product made from, what is on its surface, and has that exact blank been tested?
Plastic Is Not One Material
This is the most important difference between plastic UV printing and many other substrate categories.
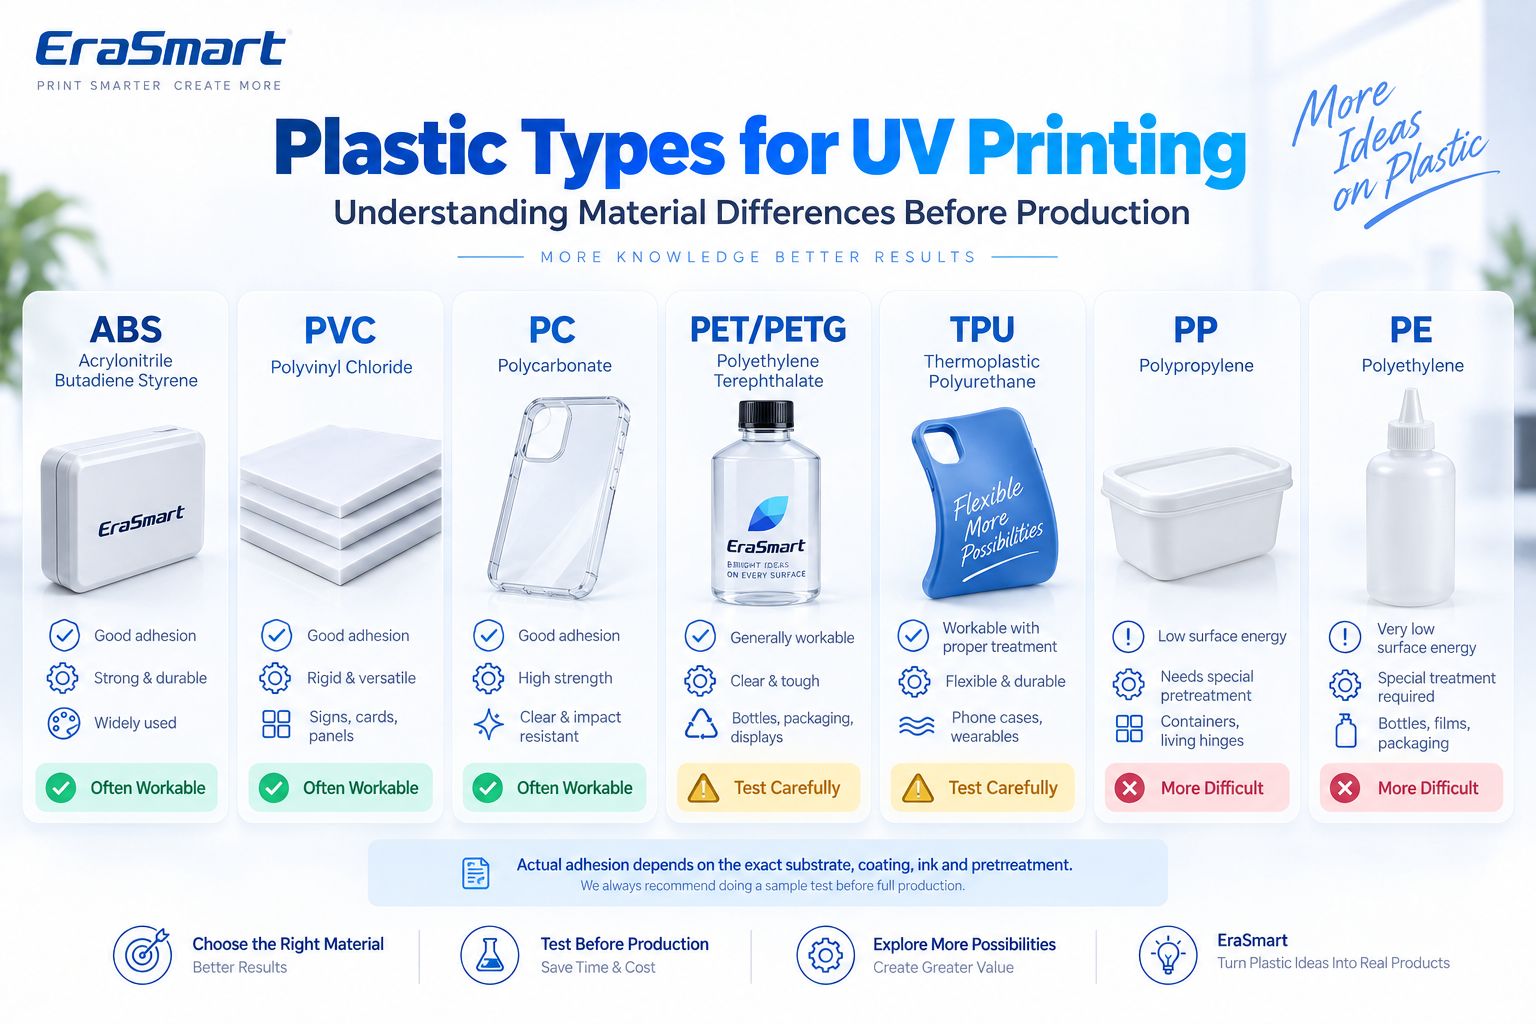
The term “plastic” covers a large family of polymers.
Different plastics can vary in:
- energia superficial
- rigidity
- flexibility
- chemical composition
- additives
- mold-release agents
- revestimentos
- transparência
- heat sensitivity
- resistência a arranhões
Even two products both labeled “ABS” may not behave identically if one contains a coating, paint, anti-static layer or mold-release residue.
That is why production approval should always be based on the actual blank, not only the polymer name.
How Does UV Printing on Plastic Work?
A UV flatbed printer jets UV-curable ink directly onto the plastic surface.
A typical process is:
- Prepare a arte.
- Import it into RIP software.
- Configure camadas CMYK, branco e verniz.
- Position the plastic product.
- Defina a altura de impressão correta.
- Print directly onto the substrate.
- A luz UV cura a tinta durante a impressão.
- Inspecione a amostra.
- Test adhesion and durability for the intended application.
UV ink does not need to soak deeply into the plastic.
Instead, the cured ink layer must maintain sufficient interaction with the plastic surface.
Isso faz surface condition and adhesion critical.
For the chemistry and curing principle, see O que é tinta UV?.
ABS Plastic
ABS, or acrylonitrile butadiene styrene, is common in:
- electronics housings
- device covers
- rigid cases
- produtos promocionais
- appliance components
- molded parts
ABS is often one of the more workable plastics for UV printing in compatible ink systems.
However, the surface may still contain:
- mold-release residue
- grease
- impressões digitais
- paint
- protective coatings
So the correct workflow remains:
clean → sample print → adhesion test
rather than assuming every ABS part can be printed without preparation.
PVC
PVC is widely used in:
- plastic cards
- sinalização
- painéis
- etiquetas
- itens promocionais
- display components
EraSmart currently lists PVC among the supported materials for its A3 PRO UV flatbed printer.
PVC can be a practical direct-print substrate, but PVC itself also varies.
There are:
- rigid PVC
- flexible PVC
- clear PVC
- colored PVC
- coated PVC
- modified formulations
Plasticizers and surface coatings can affect the final result.
Always test the actual product.
Polycarbonate / PC
Polycarbonate is used for:
- transparent panels
- electronics components
- covers
- protective products
- display parts
- clear decorative pieces
Polycarbonate can provide good adhesion with compatible UV systems, and cleaning with a suitable method is often recommended before printing to remove contamination and reduce surface issues.
Transparent polycarbonate also creates another design decision:
Do you want transparency or opaque full color?
That determines how white ink should be used.
PET and PETG
PET and PETG are common in:
- garrafas
- embalagem
- transparent displays
- containers
- sheet products
Their printing behavior depends strongly on the exact material and surface treatment.
For PET, technical UV-printing guidance specifically recommends evaluating high-adhesion surface treatment, including corona or plasma treatment, with primer considered when necessary.
That does not mean every PET product needs corona treatment.
It means PET should not be approved simply because another PET sample printed successfully.
TPU
TPU is a flexible thermoplastic commonly found in:
- flexible phone cases
- protective covers
- wearable accessories
- soft customized products
EraSmart’s A3 PRO currently lists TPU among its supported materials.
However, TPU introduces a second production question beyond adhesion:
flexibility.
A print may adhere successfully while the product lies flat but still fail after repeated:
- bending
- twisting
- stretching
- abrasão
For flexible TPU products, test the finished product under realistic movement conditions.
Direct printing success does not automatically guarantee long-term flex performance.
Polypropylene / PP
PP deserves special attention.
It is widely used for:
- containers
- embalagem
- bonés
- caixas
- household products
- molded components
But PP is commonly regarded as a more difficult surface for ink adhesion.
Technical UV-printing documentation identifies polypropylene as one of the materials where ink can be difficult to adhere reliably.
Possible solutions may include:
- compatible primer
- corona treatment
- plasma treatment
- another validated surface modification
But none of those should be assumed to work universally.
The resin grade, additives and manufacturing process still matter.
Polyethylene / PE
PE is widely used for:
- garrafas
- filmes
- bags
- containers
- embalagem
- molded products
Like PP, polyethylene is usually a higher-risk substrate for direct UV adhesion.
Technical printer documentation also identifies PE among materials that can be difficult for UV ink adhesion.
This makes PE a material that should always be approached through testing rather than marketing assumptions.
Coated Plastic
Some plastic products are:
- pintado
- lacado
- revestido
- treated
- printed with another base layer
In these cases, the UV ink may not actually be bonding directly to the polymer.
It is bonding to the revestimento.
Therefore the real substrate becomes:
plastic + coating system
A coating can improve printing in one product and create adhesion problems in another.
Why Surface Energy Matters in Plastic UV Printing
Surface energy helps explain why one plastic prints easily while another does not.
For a UV ink droplet to form a useful printed layer, it must first wet the surface sufficiently.
On a more receptive surface, the ink spreads in a controlled way.
On a difficult low-surface-energy material, the ink may:
- bead
- retract
- wet unevenly
- show weak adhesion
- peel more easily
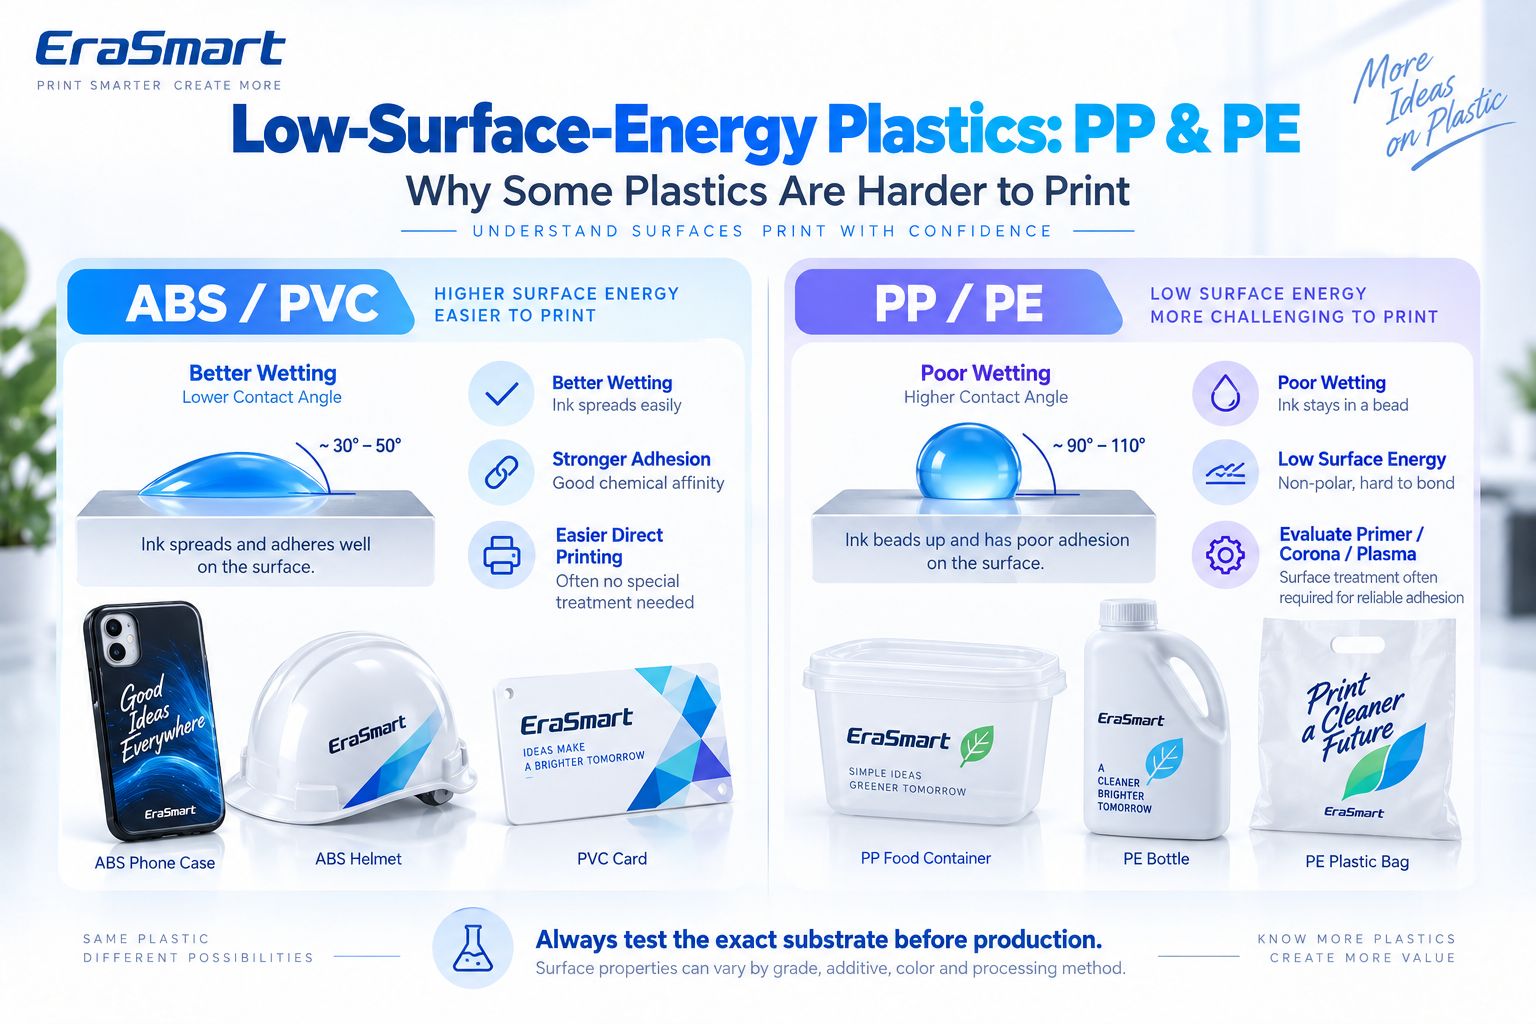
PP and PE are well-known examples of plastics that can present this type of challenge.
For production, the useful lesson is not a theoretical surface-energy number.
Isso é:
If the ink does not wet and adhere reliably, evaluate the substrate, pretreatment and ink system before changing artwork or DPI.
Why Is UV Ink Peeling Off PP or PE?
If UV ink peels easily from polypropylene or polyethylene, possible causes include:
- low surface energy
- mold-release residue
- silicone or slip additives
- óleo
- contaminação
- primário inadequado
- insufficient surface treatment
- incompatible ink/substrate combination
A common mistake is to increase UV curing and assume the problem must be “undercured ink.”
Curing and adhesion are related but not identical.
An ink layer can be cured and still have poor adhesion to the substrate.
If adhesion is weak, investigate the ink-to-plastic interface.
How to Prepare Plastic Before UV Printing
Preparation should begin before the artwork is printed.
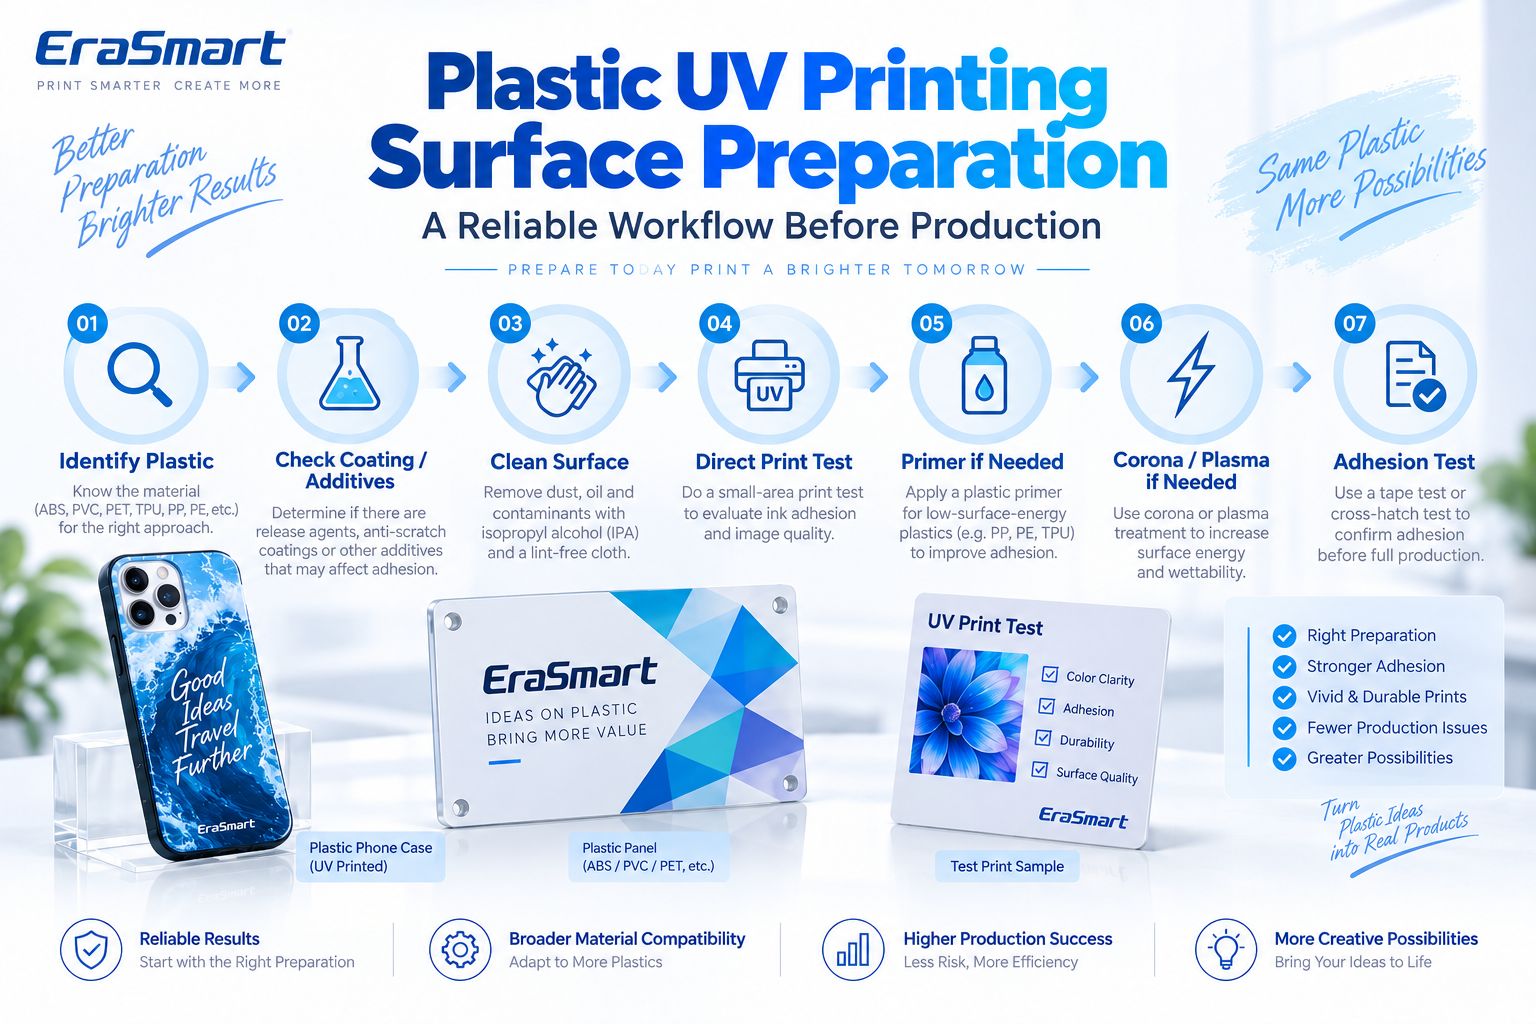
Step 1: Identify the Plastic
Determine whether it is:
- ABS
- PVC
- PC
- BICHO DE ESTIMAÇÃO
- PETG
- TPU
- PP
- PE
- another polymer
If the material is unknown, ask the blank supplier.
Step 2: Check Coatings and Additives
Procurar:
- protective coating
- paint
- mold-release residue
- anti-static treatment
- silicone
- slip additives
- surface lacquer
These can completely change adhesion behavior.
Step 3: Clean the Surface
Remover:
- pó
- óleo
- impressões digitais
- resíduo de fabricação
Use a cleaning method compatible with the actual plastic.
Do not assume the same solvent is safe for every polymer.
Some plastics can haze, crack or react with aggressive cleaners.
Step 4: Print a Small Direct Test
Before pretreating everything, test whether the surface already provides adequate adhesion.
This helps avoid unnecessary production steps.
Step 5: Evaluate Primer If Needed
If direct printing does not achieve the required adhesion, consider a compatible primer.
Primer should be selected according to:
- plástico
- Tinta UV
- intended durability
- supplier recommendations
Do not assume one universal plastic primer works on every polymer.
Step 6: Evaluate Corona or Plasma Treatment
For certain difficult substrates, surface treatment can improve printability.
Technical UV printing guidance specifically recommends evaluating corona/plasma treatment for PET films and plasma treatment for some molded plastic products.
These processes are especially relevant in higher-volume or industrial production.
They are not automatically necessary for every small print shop.
Step 7: Print a Production Sample
Use the final:
- blank
- obra de arte
- camadas de tinta
- cleaning procedure
- primer/treatment
- print settings
Etapa 8: teste de adesão
Only approve production after the sample meets the requirements of the final product.
Primer vs Corona vs Plasma: What’s the Difference?
These methods all attempt to improve print reliability, but they do not work in exactly the same way.
Cartilha
Adds a compatible intermediate layer between the substrate and UV ink.
Useful when:
- direct adhesion is inadequate
- a validated primer exists
- production volume makes the additional step practical
Corona Treatment
Modifies the surface to improve wettability.
Often associated with:
- filmes
- BICHO DE ESTIMAÇÃO
- PP
- PE
- packaging substrates
Plasma Treatment
Also modifies the surface and may be suitable for:
- molded plastics
- rigid parts
- difficult substrates
The correct method depends on your production environment.
For a custom print shop producing phone cases, a compatible prepared blank may be more practical than installing industrial surface-treatment equipment.
For a manufacturer printing thousands of molded PP parts, the calculation is different.
White Ink on Plastic
Plastic color and transparency strongly affect the final print.
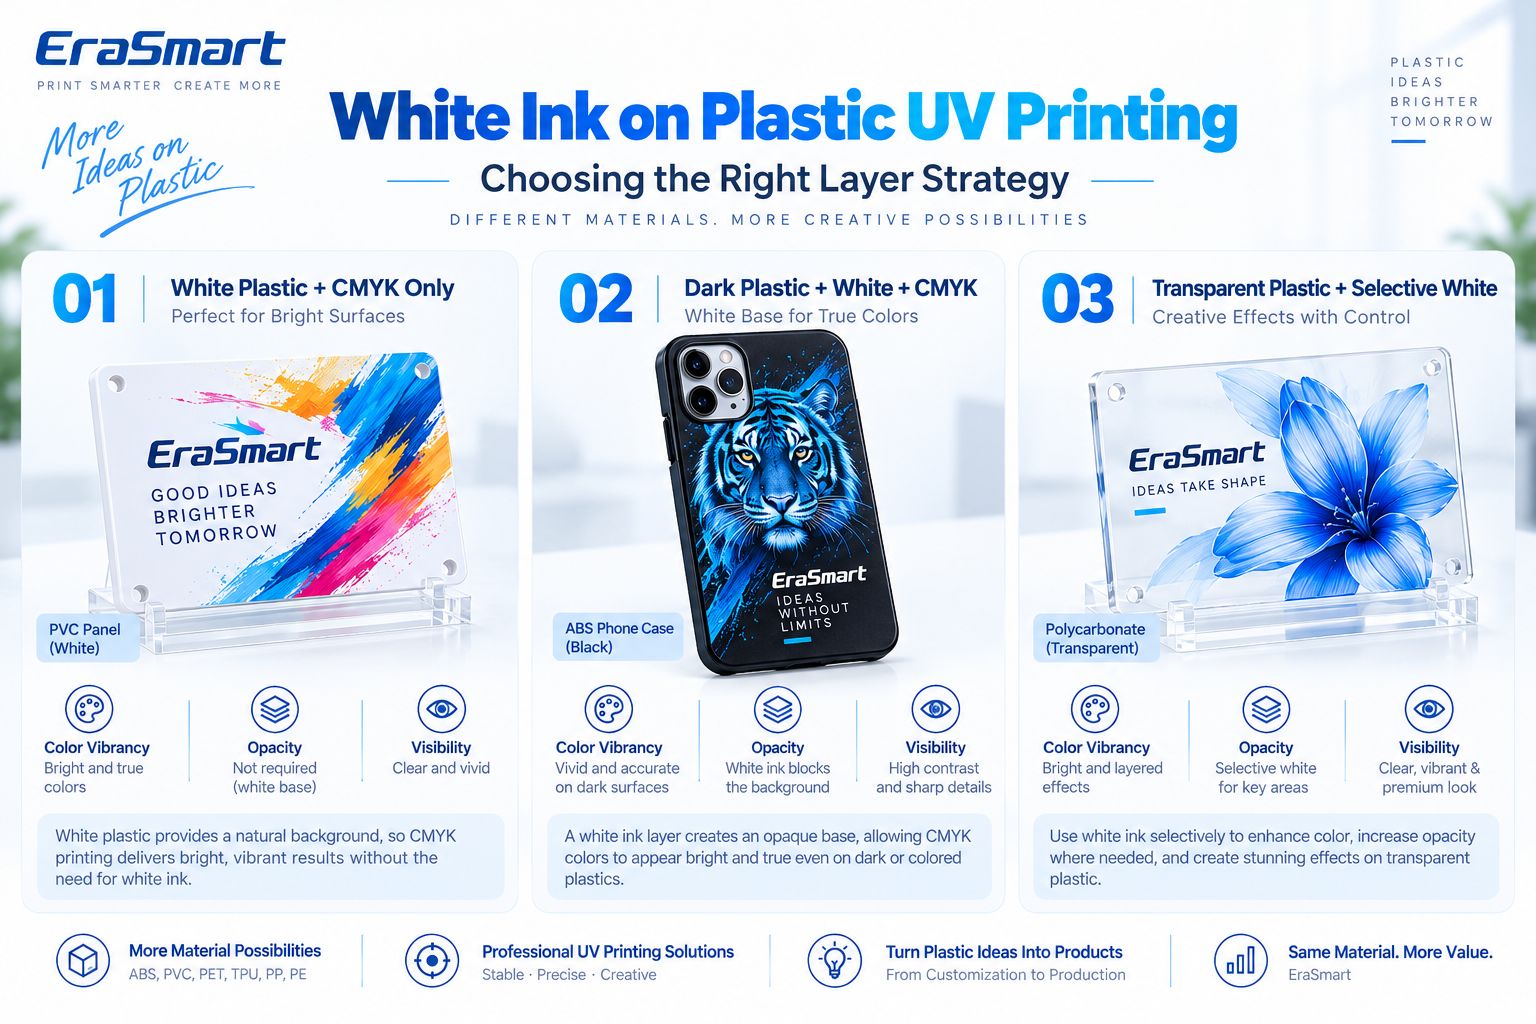
White or Light Plastic: CMYK Only
White plastic already provides a neutral visual background.
Exemplos:
- white PVC panel
- white ABS enclosure
- white plastic card
CMYK-only printing may be sufficient when opacity and design requirements allow.
Dark Plastic: White + CMYK
On:
- black ABS
- dark phone cases
- colored housings
- dark plastic panels
a white underbase helps block the substrate color.
Isso produz:
- brighter CMYK
- stronger contrast
- more predictable brand colors
- clearer small graphics
Transparent Plastic: Selective White
Transparent PC, PETG or other clear plastics can use white strategically.
Por exemplo:
- white behind the logo
- no white in transparent decorative areas
- white behind photographs
- selective opacity
This can combine:
transparent material + vivid printed graphics
in one product.
Branco + CMYK + Verniz
On compatible EraSmart systems, varnish can be used for:
- brilho pontual
- efeitos elevados
- destaques do logotipo
- textura decorativa
Varnish is a visual effect layer.
Do not automatically treat it as a universal abrasion-resistant protective coating.
How to UV Print on Plastic Step by Step
Once material compatibility has been established, create a repeatable workflow.
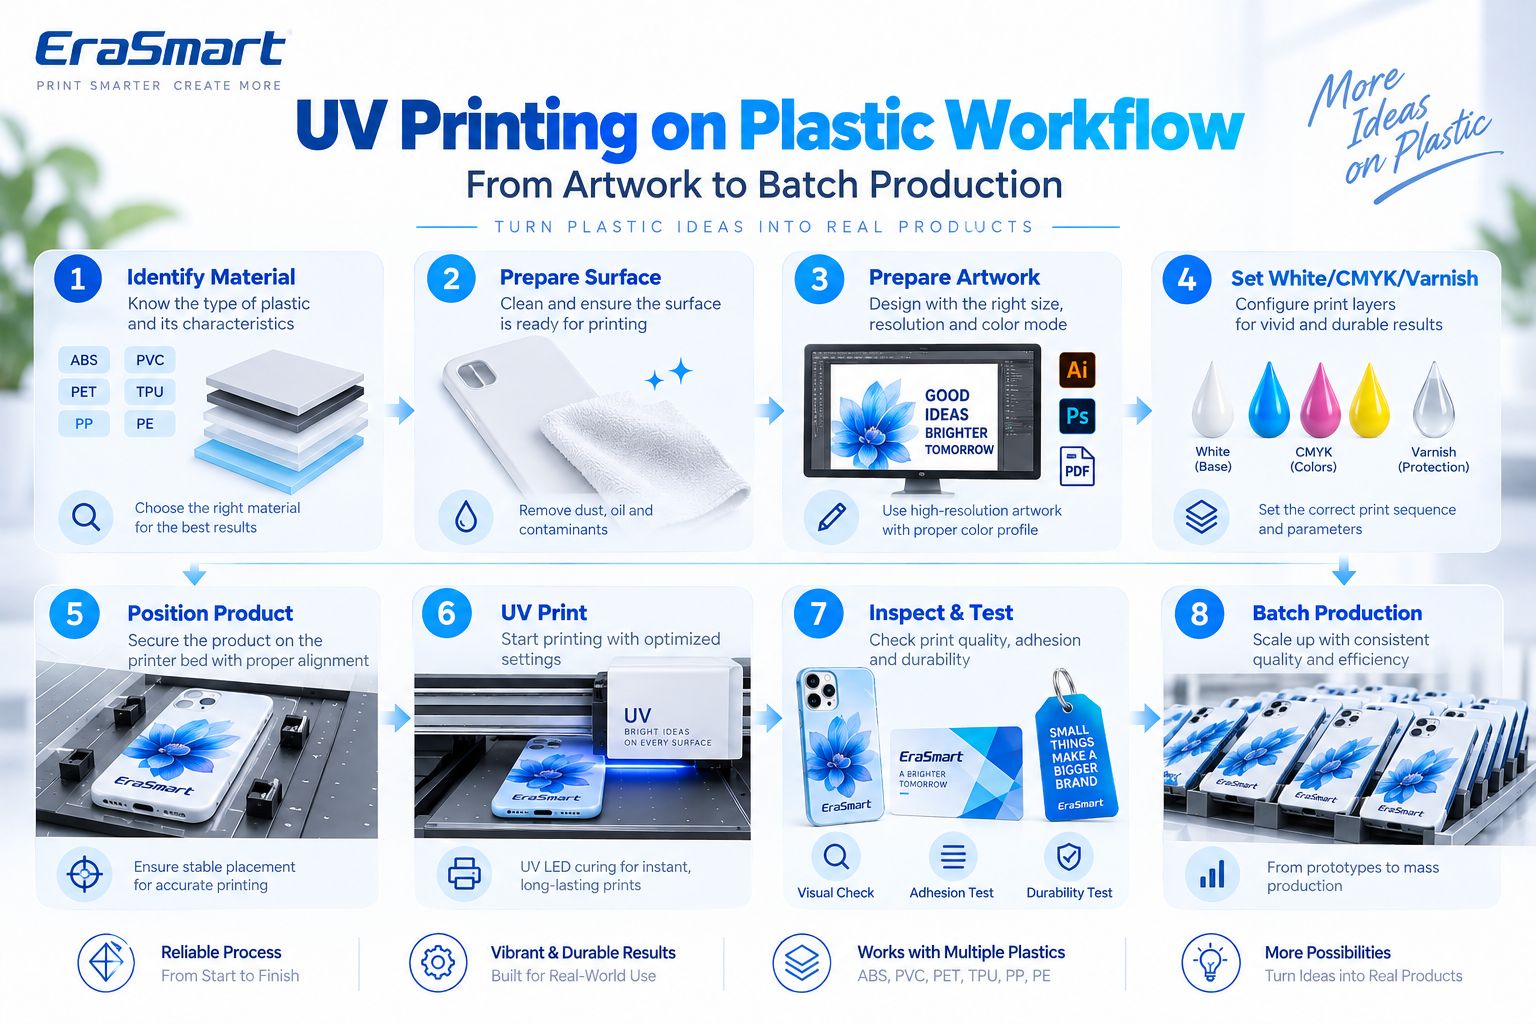
Step 1: Identify the Material
Record the actual polymer and supplier.
Step 2: Prepare the Surface
Clean and apply validated pretreatment if required.
Step 3: Prepare the Artwork
Verificar:
- dimensões finais
- resolução da imagem
- texto
- logotipos
- sangrar
- safe area
- personalização
For close-view raster artwork, around 300 DPI at final size is a practical starting point.
A arte vetorial é preferida para:
- logotipos
- texto
- Códigos QR
- gráficos de linha
Step 4: Prepare White / CMYK / Varnish
Escolher:
- Cmyk
- Branco + CMYK
- Branco Seletivo + CMYK
- Branco + CMYK + Verniz
according to the plastic color and desired effect.
Step 5: Position the Product
For repeat products such as phone cases, use:
- jogos
- gabaritos
- paradas de esquina
- modelos
Etapa 6: definir a altura de impressão
Use appropriate clearance based on the product thickness.
Etapa 7: imprimir uma amostra
Verificar:
- cor
- alinhamento
- opacidade branca
- verniz
- adesão
- product fit
Step 8: Perform Application-Specific Tests
Depending on the product, test:
- adesão
- flex
- resistência a arranhões
- manuseio
- limpeza
Step 9: Lock the Production Setup
Save:
- Predefinição de RIP
- fixture location
- material name
- supplier
- pré-tratamento
- white ink setup
Step 10: Begin Batch Production
Perform periodic QC throughout production.
How to Test UV Ink Adhesion on Plastic
A printed sample should be tested according to its real use.
Verificação básica de fricção
Útil para detectar falhas óbvias de adesão.
Verificação interna baseada em fita
Can help compare production samples.
If a customer requires a formal recognized test standard, follow that complete standard rather than treating a simple shop tape test as certification.
Avaliação de arranhões/abrasão
Útil para:
- chaveiros
- cases
- control panels
- cartões
- produtos promocionais
Flex Test
Especially important for:
- TPU
- flexible cases
- bendable components
Bend the product in a way representative of actual use and inspect whether the ink cracks or separates.
Resistência à limpeza
Útil para:
- device housings
- frequently handled items
- reusable plastic products
Test with a cleaning method that reflects the real application.
Direct UV Printing vs UV DTF on Plastic
EraSmart oferece ambos Impressoras planas UV e Impressoras UV DTF.
They solve different product-shape problems.
Impressão plana UV direta
Well suited to:
- Casos de telefone
- plastic cards
- ABS housings
- PVC panels
- flat tags
- control panels
- plastic signage
- produtos promocionais
The object is positioned directly on the printer bed.
DTF UV
Can be practical for:
- garrafas
- curved containers
- irregular finished plastic products
- difficult-to-position surfaces
But UV DTF does não eliminate surface-adhesion considerations.
A UV DTF transfer may still have poor adhesion on a low-surface-energy PP or PE product.
Always test the finished blank.
Plastic Products You Can Print with a UV Printer
Plastic is one of the broadest categories for custom-product businesses.
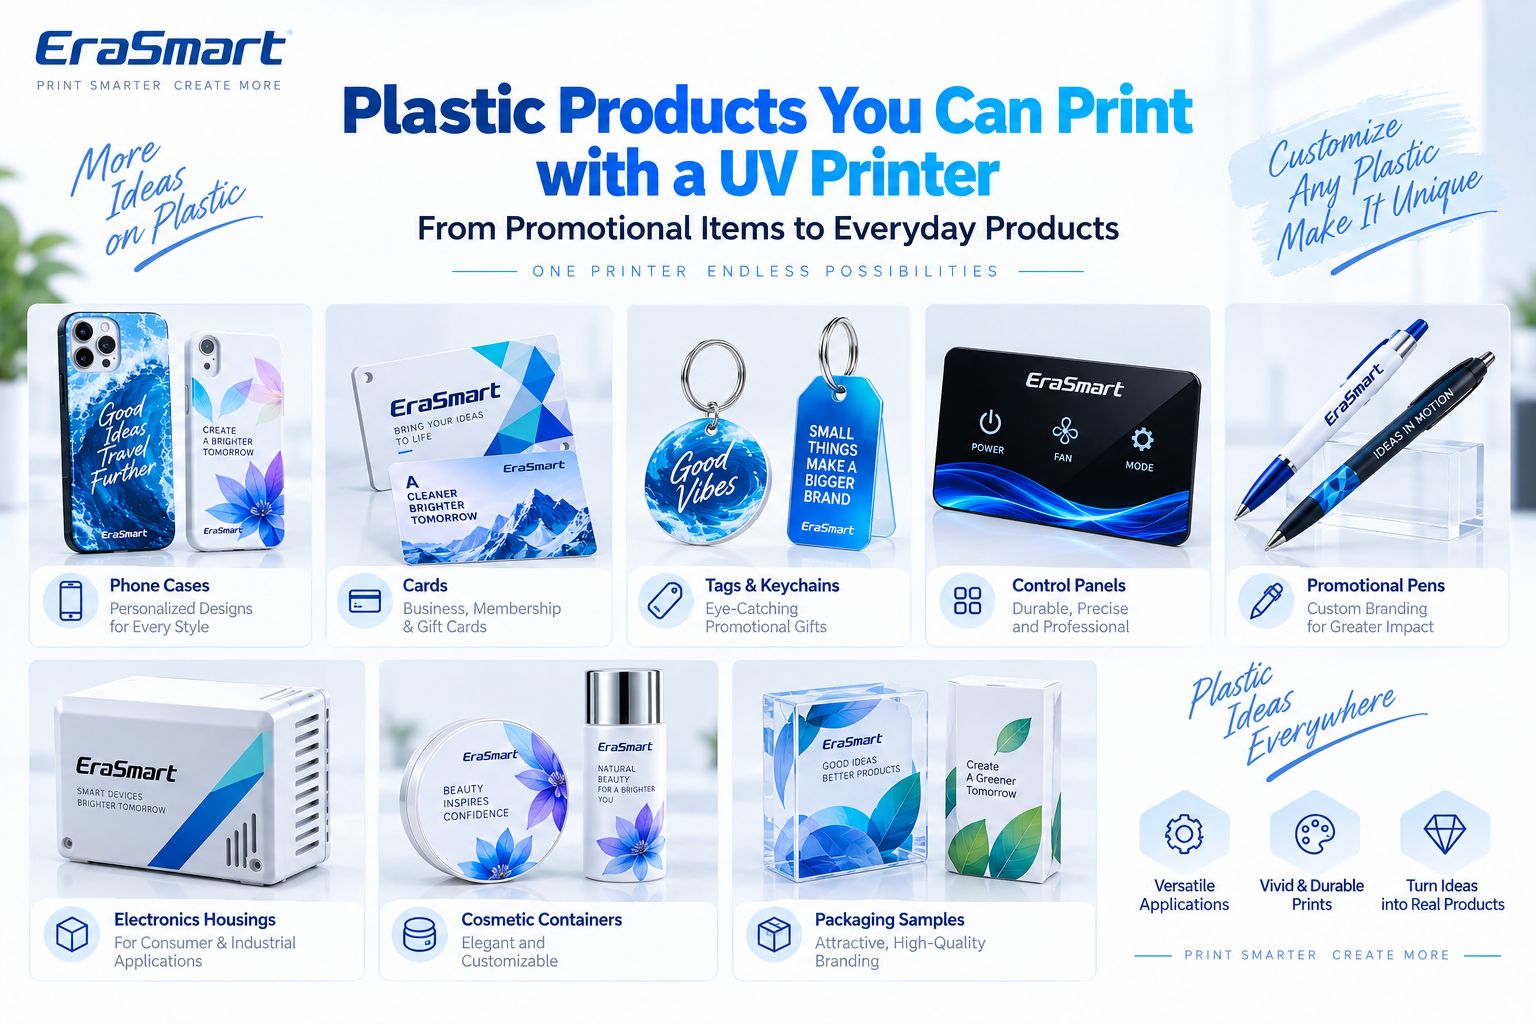
1. Capas de telefone
One of the most common small-format UV applications.
Os projetos possíveis incluem:
- fotografias
- nomes
- ilustrações
- gráficos de marca
- personalized artwork
Use a jig when printing multiple cases.
2. Plastic Cards
As aplicações incluem:
- membership cards
- gift cards
- promotional cards
- identification-style products
The exact PVC or plastic card construction should be tested.
3. Tags and Keychains
Útil para:
- brindes promocionais
- mercadoria de evento
- souvenirs
- personalized products
4. Electronics Housings
Os produtos possíveis incluem:
- small device covers
- remote housings
- painéis de equipamentos
- control components
Check whether the housing contains surface coatings or mold-release residue.
5. Control Panels
A impressão UV pode adicionar:
- ícones
- operating instructions
- branding
- interface graphics
If the panel is part of a regulated industrial product, the final assembly must meet the applicable requirements; decorative UV printing alone does not establish compliance.
6. Promotional Products
Os exemplos incluem:
- canetas
- cases
- small accessories
- giveaways
- branded parts
7. Cosmetic Containers
Certain compatible containers can be customized with:
- logotipos
- graphics
- marca do produto
Curved containers may be better suited to UV DTF or an appropriate rotary workflow.
8. Packaging Samples
UV printing can be useful for:
- prototypes
- short-run samples
- marketing mockups
- product-launch packaging
9. Plastic Panels and Signs
Common materials include compatible:
- PVC
- polycarbonate
- coated plastic panels
Which EraSmart UV Printer Is Suitable for Plastic?
For small and medium flat plastic products, the Impressora UV EraSmart Digital Inkjet A3 – Dual XP600 is one practical option.
Current specifications include:
| Especificação | EraSmart A3 PRO |
|---|---|
| Cabeças de impressão | XP600 duplo |
| Área de impressão | 350 × 450 milímetros |
| Altura de impressão | 0–130mm |
| Resolução | Até 1440 dpi |
| Configuração de tinta | CMYK + WW + VVVVVV |
| Circulação de tinta branca | Sim |
| Limpeza Automática | Sim |
| Plataforma de sucção | Sim |
| Medição de Altura | Infravermelho |
| RASGAR | Riin / PrivateRip |
EraSmart currently lists PVC, TPU and phone cases among the supported materials and applications. The product page also explicitly notes that some plastics and low-surface-energy materials may perform better with coated blanks or primers.
This makes it suitable for evaluating products such as:
- Casos de telefone
- PVC cards
- etiquetas
- plastic panels
- small housings
- produtos promocionais
- other flat plastic handicrafts
The important point is that the printer provides the printing platform.
Material compatibility still needs to be validated on the actual plastic.
Why Jigs Matter for Plastic Production
Plastic products are often manufactured to repeatable dimensions.
That makes them excellent candidates for jigs.
Suppose a customer orders 100 phone cases.
Instead of positioning each case manually:
- Create a fixed jig.
- Place several cases in repeatable positions.
- Lock X/Y coordinates.
- Save the RIP layout.
- Print an approved sample.
- Repeat the process.
This improves:
- registro
- velocidade de produção
- consistência
- personalization efficiency
Common Problems When UV Printing on Plastic
Ink Peels Off Easily
Verificar:
- polymer type
- óleo
- mold-release residue
- low surface energy
- revestimento
- cartilha
- tratamento de superfície
Do not assume the problem is DPI.
Ink Beads on the Surface
This can indicate poor wetting.
Considerar:
- contaminação
- low surface energy
- inappropriate substrate
- tratamento de superfície
Colors Look Weak on Dark Plastic
Use an appropriate white underbase.
Transparent Plastic Looks Washed Out
Considerar:
- Branco + CMYK
- branco seletivo
- backing layer
depending on the desired appearance.
TPU Print Cracks When Bent
The issue may be ink-film flexibility rather than initial adhesion.
Test the real bending conditions.
A tinta branca parece irregular
Verificar:
- circulação
- condição do bico
- RIP configurações de branco
- manutenção de impressora
Product Position Changes
Use a fixture instead of placing each product by eye.
Surface Becomes Damaged During Cleaning
The cleaning method may be too aggressive for that plastic.
Always confirm chemical compatibility before production.
Limites de segurança e aplicação
Plastic UV printing also requires application-specific judgment.
Food Contact
Do not assume standard decorative UV ink is suitable for direct food-contact surfaces.
For food packaging or containers, printing should remain within the validated design and compliance requirements of the finished product.
Children’s Products
Products intended for children may be subject to specific chemical and safety requirements.
Printing compatibility does not establish product compliance.
Medical Products
Do not treat general UV printing as automatically suitable for medical-device contact surfaces.
Flexible Products
Successful printing on TPU or another flexible polymer does not automatically mean unlimited stretch resistance.
Uso ao ar livre
A durabilidade ao ar livre depende de:
- resina
- revestimento
- Tinta UV
- adesão
- exposição ambiental
- abrasão
Teste o produto acabado antes de fazer alegações de vida útil ao ar livre.
How to Choose a UV Printer for Plastic Products
Before buying a printer, identify your real product mix.
What Plastic Are You Printing?
ABS, PVC and PP can require very different workflows.
O produto é plano?
Produtos planos são a escolha natural para impressão plana UV.
Is It Dark or Transparent?
This determines white ink requirements.
Is It Flexible?
If yes, test flex performance.
Is It Low Surface Energy?
PP and PE deserve extra caution.
Is It Curved?
Consider UV DTF or an appropriate rotary workflow.
Will You Print the Same Product Repeatedly?
If yes, plan for:
- gabaritos
- batch layouts
- saved presets
- material records
- repeatable pretreatment
Final Answer: Is UV Printing Good for Plastic?
Yes—but plastic must be treated as a family of different materials rather than one universal substrate.
ABS, PVC and some polycarbonate products can often provide workable surfaces.
PET and TPU require closer evaluation.
PP and PE are generally higher-risk materials for direct UV adhesion and may require additional pretreatment or purpose-made printable blanks.
The reliable workflow is:
Identify → Clean → Direct Test → Pretreat If Needed → Print Sample → Test Adhesion → Test Real Use → Standardize → Produce
Usar:
- Somente CMYK on suitable white/light plastic
- Branco + CMYK on dark plastic
- Branco Seletivo + CMYK on transparent plastic
- Verniz for selected premium visual effects
- Mesa UV for suitable flat products
- DTF UV for certain curved or difficult-to-position products
For flat plastic customization, explore the Impressora UV EraSmart faixa.
For curved plastic bottles, containers and irregular products, compare the Impressora EraSmart UV DTF fluxo de trabalho.
Perguntas frequentes
Can a UV printer print directly on plastic?
Yes. Many plastics can be directly UV printed, but compatibility and adhesion depend on the exact polymer, surface treatment and ink system.
What plastics are easiest to UV print?
ABS, PVC and polycarbonate are commonly workable in compatible UV-printing systems, but every finished product should still be tested.
Can you UV print on polypropylene?
Potentially, but PP is a more challenging low-surface-energy substrate and may require a validated primer or surface treatment.
Can you UV print on polyethylene?
Potentially, but PE is also a difficult adhesion substrate and should be carefully tested before production.
Can you UV print on PET?
Yes, depending on the PET surface. Some PET products benefit from corona/plasma or other high-adhesion surface treatment.
Can an EraSmart UV printer print PVC?
Yes. PVC is explicitly listed among the supported materials for the EraSmart A3 PRO.
Can an EraSmart UV printer print TPU?
Yes, TPU is also listed among the supported materials, but flexible applications should be tested under realistic bending conditions.
Do I need primer for plastic UV printing?
Not always. Primer depends on the plastic, surface energy, coating, UV ink and required adhesion.
Why does UV ink peel off plastic?
Possible causes include contamination, mold-release residue, low surface energy, incompatible coating, unsuitable pretreatment or an incompatible ink/substrate combination.
Do I need white ink on plastic?
White ink is especially useful on dark, colored and transparent plastics. White plastic may not require a full white underbase.
Can I UV print phone cases?
Yes. Phone cases are a common flatbed UV application, but the exact case material and coating should be tested.
Can I UV print plastic bottles?
For curved bottles, UV DTF or an appropriate rotary workflow may be more practical than standard flatbed direct printing.
Which EraSmart UV printer is suitable for plastic products?
O EraSmart A3 PRO Dual XP600 provides a 350 × 450 mm working area, 0–130 mm print height and CMYK + white + varnish configuration for flat personalized products.
Build a Reliable Plastic Printing Workflow
If you are evaluating a UV printer for plastic products, tell EraSmart:
- plastic type
- dimensões do produto
- rigid or flexible
- dark / white / transparent
- coated or uncoated
- flat or curved
- volume mensal esperado
- whether white ink is required
- whether varnish is required
Our team can help you evaluate the appropriate Impressora UV EraSmart ou Impressora UV DTF workflow for your actual plastic products.
Pode ser você também
Copyright 2020 © Erasmart. | Sitemap